John Finlay Group Of Companies

Aadil Keshwani

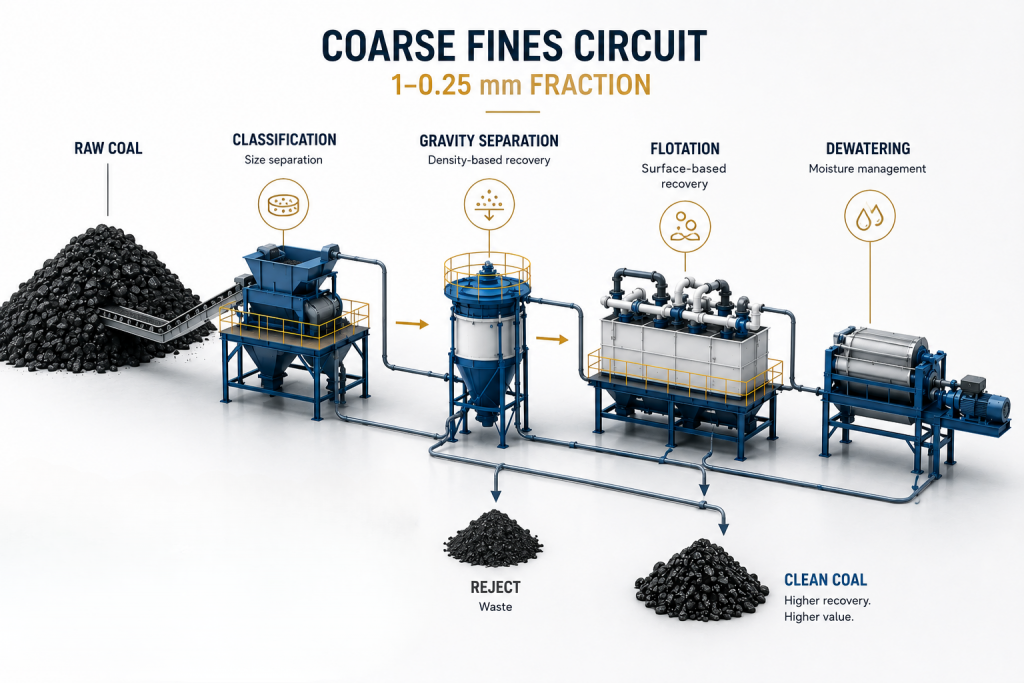
Coal-Beneficiation-circuit-Flowchart-diagram

The 1–0.25 mm Fraction in Indian Coal Washeries

A technical perspective on coarse fines separation, project economics, and circuit selection in Indian coal beneficiation There is a renewed debate in the Indian coal processing industry around the 1–0.25 mm fraction — often called the “coarse fines” fraction. The argument usually follows a simple line:Indian washeries are leaving yield on the table in this size range. HydroFloat coarse-particle flotation can recover that yield. Therefore, Indian operators are commercially behind for not adopting it. The first part of that argument is directionally correct. The 1–0.25 mm fraction is important, and in many washeries it deserves more attention than it receives. The conclusion, however, is too simple. The correct question is not“Why has India not adopted HydroFloat?” The correct question is:“For this coal, this size distribution, this NGM profile, this oxidation condition, this existing circuit, and this capital envelope, which separator gives the best project economics?” That is a very different engineering question. Our group has executed 130+ EPC washery projects globally and currently operates 47 plants. Across Indian, Chinese, Australian, and African coals, the 1–0.25 mm fraction has repeatedly proven to be one of the highest-leverage areas in washery design. But it is also one of the easiest areas to oversimplify. The technology decision should be made on physics, operating data, and full-circuit economics — not on the comparative sales narrative of any single equipment supplier. By Aadil KeshwaniManaging Director, John Finlay India Pvt. Ltd. 1. The Yield Math Needs the Right Denominator A commonly repeated claim is that a 2–3% additional recovery in the 1–0.25 mm fraction can translate into 20,000–30,000 tonnes of additional clean coal per year in a 1 MTPA washery. That number needs careful qualification. A 1 MTPA washery does not process 1 million tonnes per year of 1–0.25 mm material. In many Indian coking coal washeries, this fraction is typically a minority of total ROM feed. The exact number depends on top size, crusher product, seam characteristics, friability, and fines generation. Therefore, a recovery improvement inside the 1–0.25 mm fraction cannot be directly treated as the same percentage improvement in total plant yield. For example, if the 1–0.25 mm fraction represents around 15–25% of total feed, then even a meaningful recovery improvement within that fraction translates into a much smaller plant-level uplift. This does not mean the gain is unimportant. A one-percentage-point improvement in overall clean coal yield can be very valuable in the right plant. But the commercial case must be built on the corrected denominator. The honest calculation is:fraction mass × realistic recovery improvement × clean coal valueminus incremental CapExminus incremental OpExminus operating risk That is the calculation that matters. If a technology claims 2–3 percentage points of total plant yield improvement, then it should be supported by plant data. If the claim is 2–3% improvement within the coarse-fines fraction, then the plant-level gain is much smaller. This distinction is not academic. It determines whether the payback is compelling, marginal, or uneconomic. 2. Coarse-Particle Flotation Works — But It Has Physical Limits HydroFloat is good engineering. The principle of fluidised-bed coarse-particle flotation is sound. By reducing turbulence in the bubble-particle contact zone, the technology can extend flotation beyond the range where conventional mechanical cells become inefficient. In the right mineral systems, this is a powerful advantage. But coarse-particle flotation is still limited by bubble-particle stability. As particle size increases, the forces that detach a particle from a bubble rise faster than the forces holding the particle to the bubble. HydroFloat reduces turbulent detachment, but it does not eliminate gravity, inertia, particle shape effects, incomplete liberation, or surface oxidation. In practical coal terms:Below 1 mm, HydroFloat can perform well on liberated, hydrophobic coal. Between 1.0 and 1.5 mm, performance becomes more coal-specific. Above that range, recovery is increasingly dependent on liberation, density, surface condition, and particle-bubble stability. This does not make HydroFloat ineffective. It simply means the technology should not be treated as a universal answer for the full 1–0.25 mm coal fraction. For coal, the right comparison is not HydroFloat versus a poorly operated legacy fines circuit. The right comparison is HydroFloat versus a properly specified gravity circuit: TBS, Reflux Classifier, small-diameter dense medium cyclone, or a combination of these. That comparison is much closer. 3. Reagent OpEx Cannot Be Treated as a Footnote Any flotation-based circuit has a reagent dependency. In Indian coal, that dependency matters. A HydroFloat circuit requires collector, frother, conditioning, reagent dosing, air supply, froth handling, instrumentation, and additional operating attention. These are not minor items when the incremental yield gain is being measured against only a fraction of total plant feed. The reagent cost may be manageable in some applications. But it must be included honestly in the economic model. Indian coking coal adds another complication: variable oxidation. Coal that has been stored, weathered, blended across seams, or exposed to monsoon conditions can show significant variation in surface hydrophobicity. As oxidation increases, flotation response becomes less predictable and reagent consumption can rise materially. This is one of the recurring reasons why flotation circuits in Indian coking coal do not always achieve design recovery in sustained operation. Gravity circuits are not immune to poor operation. They require classification discipline, water balance, density control, and mechanical maintenance. But their failure modes are different. A TBS, Reflux Classifier, or dense medium cyclone does not require the coal surface to remain consistently hydrophobic. It separates primarily on density and settling behavior. That distinction matters in India. 4. The CapEx Comparison Must Be Scope-Based The capital comparison also needs to be made carefully. A HydroFloat installation for this duty is not just a cell. The installed system may include classification, conditioning tanks, reagent storage and dosing, air systems, froth pumps, launders, instrumentation, civil works, and downstream dewatering modifications. Depending on site conditions and import content, the installed cost can be materially higher than a TBS circuit and often higher than a Reflux Classifier circuit. That does not automatically make HydroFloat uneconomic. If the yield gain is large enough, the payback can justify
The 1–0.25 mm Fraction in Indian Coal Washeries Read More »

Centrifuge Maintenance Information

FLL-1500WZ Centrifuge Information about the main parameters of the device The user   The manufacturer John Finlay Model FLL-1500WZ Usage Dewater Series No FE02-24014 / JFE02-24015 Weight 11754 kg Basket Hefei John Finlay Mining Equipment Pty. Ltd. Equipment dimensions 3310mm * 3165mm * 2192mm Drive motors 75kW,380/660V,IP55,P6,3PH,50Hz vibration motor vibration motor     415 V, the vibration motor is 8.4 kW,IP65,P4,3PH,50Hz Lubricating machine 0.75kW,380/660V,IP55,P4,3PH,50Hz Cycle Contents Operation  Notes weekly Check the oil mark Routine inspection of oil quality Check the scale of the filter If necessary, it will be raised If necessary, replace it   Clean or replace the oil filter   Monthly “Y” filter Vibrating motors   Lubricating oil circuit and configuration Vibrating motors   Transmission belts cleanup Lubricate the motor – check the Condition of the stroke pointer Routine inspections, if necessary, repairs   Check that the M36 bolts on the two vibrating motors are No fastening Re-tensioning – every 3.5-5.1 kg force required 20mm bending.           Every 3 months Lubrication of Bearings on shafts Main bearings Replace the automatic oiler on the spindle bearing Check the adjusting bearings   Half year Bolts from the water tank to the sub-cube Shaft inlet part/polyurethane cover Check the condition, replace it if  it is old or deformed Check if necessary repairs Check the internal and external conditions    Basket replacement basket holder   The lining of the discharge section Infeed chute Check the condition, replace it if  it is old or deformed Check if necessary on repairs Check the internal and external conditions    Notes: Lubrication schedule Specification  Lubricating oil sepcification Lubricating oil quantity Hours 75KW driving motor,6 poles L-XBCHA3 45g 3000-4000 0.75KWLubricating machine,4poles N.A- -Pre-oiled and sealed     Vibrating motors LGHP2 High-temperature grease 60g 500 fuel tank: Refueling for the first time Refueling afterwards Shell  pressure-resistant S2-G100   38-40L   38-40L   500   2000 Spindle shaft oil seal   Automatic lubricator SL-01   3 months (adjustable) Precautions It is strictly forbidden to weld, cut and do other hot operations on the water tank body to prevent the tiles and wear-resistant mud from falling off. Before the operation of the equipment, the rotation direction of the vibration motor should be checked, and the rotation direction must be reversed. The basket should be cleaned before the operation of the equipment to prevent the basket or equipment from shaking

Centrifuge Maintenance Information Read More »

Coal Preparation Plant

Thermal COAL WASHERY PLANT: Understanding the Process

In the dynamic realm of energy production, thermal coal remains a cornerstone, powering countless power plants globally. Yet, amid escalating environmental concerns, the quest for cleaner, more efficient coal processing methods intensifies. Welcome to the coal washery plant process – a transformative approach tailored for thermal coal, aimed at bolstering efficiency and sustainability. Let’s delve into the intricacies of the coal washery plant process, emphasizing its significance in optimizing thermal coal utilization while minimizing environmental impact. Understanding the Essence of the Coal Washery Plant Process The essence of the Coal Washery Plant Process lies in its ability to refine raw coal, elevating its economic value and environmental compatibility. By reducing mineral impurities, such as overburden, and ash content, the Coal Washery Plant Process ensures cleaner, more sustainable energy generation. Evolution of Coal Beneficiation Techniques Traditionally, coal was supplied in lumps for domestic and industrial use, with fines being disregarded. However, as demand surged, sophisticated handling and screening facilities emerged to cater to diverse market needs. The evolution of washing techniques, dating back to Europe in 1918 with the introduction of the “Chance” washer, underscores the continuous refinement of coal preparation methods. Understanding Indian Coal: Challenges and Opportunities Indian coals, primarily of drift origin (Gondwana Coal), pose unique challenges in coal washing due to their high ash content and the dissemination of impurities within the coal bed. Characterized by very thin bands (5 mm–3 cm) of impurities interspersed between coal bands, these coals exhibit high near-gravity material (NGM > 30%) content. It is observed that there is +/- (0.10) NGM % in the Indian Coal. The liberation size of coal is significantly smaller, with notable improvements in yield observed when coal is crushed down to as low as −6 mm to −3 mm and −1 mm. However, operating a coal washery plant with such small coal sizes is currently unfeasible under prevailing techno-economic conditions. Indian industries often perceive Indian coal as inferior to imported coal primarily due to its high ash content. However, Indian coal possesses several inherent qualities that warrant closer examination. Despite its high ash content, Indian coal exhibits low sulfur (0.2%–0.7%), low iron, low chlorine, and low toxic/rare earth elements content. Moreover, it is characterized by macerals rich coal with high ash fusion temperature and the refractory nature of silica and alumina-rich ash. These attributes underscore the untapped potential of Indian coal and call for dedicated research into coal-washing technologies tailored specifically for Indian coal. John Finlay’s Research John Finlay’s experiments on Indian coal have provided invaluable insights into optimizing coal-washing processes. Through meticulous experimentation, Finlay has concluded that washing the −13 + 1 mm fraction in Heavy Media Cyclone, the −1 + 0.106 mm fraction in spiral concentrator, and the −0.106 mm fraction in flotation cells yield superior results compared to conventional practices such as washing the −13 + 0.5 mm fraction in HM Cyclone. This revelation highlights the potential for improving coal-washing efficiency and product quality in India. Overcoming Challenges in Indian Coal Beneficiation Addressing the complexities of Indian coal beneficiation requires innovative approaches and advanced techniques. While the high near-gravity material (NGM) content presents a formidable challenge, modern coal washery technologies offer promising solutions. By leveraging techniques such as: Indian coal washeries can overcome the challenges posed by high NGM content and small liberation size, thereby improving yield and organic efficiency. Key Components of Coal Preparation Coal preparation encompasses a series of critical steps, including blending, size reduction, grinding, screening, and handling. Central to this process is coal beneficiation/coal washery plant or cleaning, aimed at optimizing coal quality and marketability. The degree of beneficiation required is contingent upon market demand, influencing the cost and methods employed. Optimizing the Coal Beneficiation Process Efficiency and sustainability are central to optimizing the Coal Washery Process. This entails: Washability Test: A Crucial Analysis Central to the Coal Washery Process is the washability test, offering insights into coal separation characteristics. By analyzing float and sink fractions, operators can determine optimal operating conditions and plant design parameters. Float and Sink Method: An Analytical Technique In the float and sink method, coal samples are subjected to sequential tests with varying-density liquids. This method enables the separation of coal and impurities based on specific gravity differences, facilitating optimal cleaning and product quality. Harnessing Modern Wash Plant Technologies Modern wash plants employ advanced techniques and ensure optimum organic efficiency. Organic Efficiency depends on the process adopted and fully depends on the process equipment employed for the beneficiation. John Finlay’s Heavy Media Cyclones provides best EP values in the Industry. Conclusion: Driving Innovation in Thermal Coal Utilization As the global energy landscape evolves, the Coal Washery Process emerges as a linchpin in enhancing efficiency and sustainability in thermal coal utilization. By optimizing coal quality and minimizing environmental impact, the Coal Beneficiation Process paves the way for a cleaner, more sustainable energy future. In conclusion, the Coal Washery Process stands as a beacon of innovation, driving positive change in thermal coal utilization. Through continuous refinement and adoption of advanced technologies, we can unlock the full potential of thermal coal as a reliable and sustainable energy source for generations to come. We recommend you check out John Finlay’s Coal Washery process equipment which is used for Coal washeries. We provide a wide range of equipment like Heavy Media Cyclones, Classifying Cyclones, and Vibrating screens. For Dry sorting equipment which uses no water to sort clean coal check out Dry Coal Sorting Equipments.

Thermal COAL WASHERY PLANT: Understanding the Process Read More »

How to OPTIMIZE CLEAN COAL YIELD

How to OPTIMIZE CLEAN COAL YIELD AT LOWER ASH% FOR COKING COAL

By Om Prakash & Aadil Keshwani: Indian coking coal reserves are depleting rapidly. Coking coal is invaluable, with washed coal vital for coke preparation, a key component in steelmaking. This paper explores optimizing clean coal yield with lower ash percentages through advanced beneficiation equipment and newly developed requisites such as reagents and flocculants. 1. Today coking coal washeries are to follow the most modern coal beneficiation technology to optimize the clean coal yield % at lower ash%. The state-of-the-art technology flow sheet for coking coal is depicted below Mostly prepared feed size range (-) 50 mm (+) 0.5 mm is beneficiated through two stages of Heavy Media Cyclone. This ensures the least percentage of misplacement of materials which adds to clean coal yield. If the laboratory test supports, then the following stages of washing can be adopted. Size Fraction                        Process Route  (-) 50 mm (+) 1.5 mm                      by Heavy Media Cyclones (-) 1.5 mm (+) 0.5 mm                     by Spiral Concentrators (-) 0.5 mm                                          by Flotation.  The de-slimed feed (-) 0.5 mm is subjected to fine beneficiation circuit. By introducing a pulp density adjusting tank between conditioner and flotation will be a good measure to maintain optimum pulp flotation density. To optimize the flotation reagents consumption normally the pulp conditioning is done at 30% solid by weight then after that conditioned pulp is diluted to required flotation density around 10% solid by weight. This adjustment is taken care of by Pulp Density Adjusting Tank. By adopting this route clean coal yield can be optimized 2. Use of most efficient JFE design Heavy Media Cyclones which can guarantee the lowest imperfection values. 3. DSM Design JFE HM Cyclones are a much better option to ensure higher efficiencies 4. Use of most efficient DSM design hydro cyclones which can guarantee the lowest imperfection values. JFE Hydro cyclones are most efficient. For classification and thickening process, the JFE design hydro cyclone battery is very helpful prior to the thickener. This helps in optimizing thickener size and good process water in recirculation in the circuit. 5. Use of efficient Magnetic Separators with required gauss strength for HMC circuit will guarantee the lowest magnetite consumption i.e. 800 grams per tonne of ROM coal. This low-intensity wet Magnetic Separator is a very long magnetic pick-up zone. This is very efficient for dense media recovery. 6. Use of Spiral Concentrator for size fraction (-) 1.5 mm (+) 0.5 mm helps in optimizing the yield of clean coal at low ash%. Spirals are: 7. Use of a Flotation System can add on yield of clean owing to the following features: 8. Use of Inclined Plate Settlers- IPS by which clarification is achieved when upstream velocity is low enough to allow solids to report to the inclined plates by using latest developed flocculent Inclined Plate Settlers have many practical advantages. 9. Use of the latest design fines clean coal dewatering devices like Pressure Filter/ Horizontal Vacuum Belt Filter which adds GCV on the product. The driving force of this filtration method is the pressure differential across the cake. A higher-pressure drop will give a faster dewatering rate and a lower residual moisture, as smaller voids are emptied from liquid.  Service and maintenance requirements are low for Pressure Filter. Hence the least downtime which helps in betterment of yield of clean coal.   10. The use of Belt Filter Press for fine-tiling dewatering investment is justified. Belt Filter Press remains a preferred technology for dewatering of fine tailing from coal washery. 11. By using instruments to measure the yield and the underflow and overflow medium densities and how the data can be used to optimize the operation of the heavy media cyclones. This can also be one of the appreciable efforts to optimize the yield of clean coal at lower ash%. 12. Use of the right quality and granulometry of magnetite in case of heavy media separators. Specification of ground magnetite for Heavy Media Cyclone Circuit: Specification of Magnetite Content                                              Specification             Fe3O4 (Magnetite Content)             98.5%             Specific Gravity                                  4.90-5.15             Particle Size                                        90% passing 45 Microns.             Fe Content                                          68-70% By use of right quality and ground size of magnetite in the heavy media circuit the maintenance of consistent cut point can be ensured which is mostly helpful for the coal feed having high +/- 0.10 NGM %. This is also a step towards optimization clean coal yield. Specification of reagents and flocculent Use of proper flotation reagents in place of conventional frother and collector can add value in the yield of clean coal. Nalco Water flotation reagents for frother and collector has established an excellent result in coal flotation industries. Conventional Reagents & Flocculent        Latest Developed Reagents &Flocculent                                                                                     By NALCO WATER Frother- Pine Oil                                                      Frother- N 9840 Collector- Diesel Oil                                                 Collector- N 88001 Thickener Flocculent-Alum                                    Thickener Flocculent-Anionic- A83384 Cationic- A102 Plus    Conclusion: By using most modern design of equipment items installed in the coal beneficiation plants can play a vital role for optimizing yield of clean coal at lower ash %. Similarly, by using the required grade of magnetite for Heavy Media Circuit, latest developed flotation reagents and flocculants for settling aids yield of clean coal can be very well optimized in the coal beneficiation plants. Coking coal deposits for our country are very limited and washed coking coal should be used judiciously. A good number of fine coal beneficiation circuits are installed in BCCL and CCL but most of fine coking coal beneficiation circuits are not in operation. By making these fine circuits operational we gain heavily on clean coal yield and steel sectors can reduce the import of coking coal. References: About Authors: Om Prakash obtained his Master of Technology from IIT Kharagpur (India) in Mineral Engineering with a specialization in Coal Preparation in the year 1979 followed by a Postgraduate in Business Administration from Pondicherry Central University. He has been closely associated with the Denver USA technology for Coal Flotation, Separator Poland, and Fives Cail Babcock France technologies

How to OPTIMIZE CLEAN COAL YIELD AT LOWER ASH% FOR COKING COAL Read More »

Metallurgy

IME Exhibition 2023

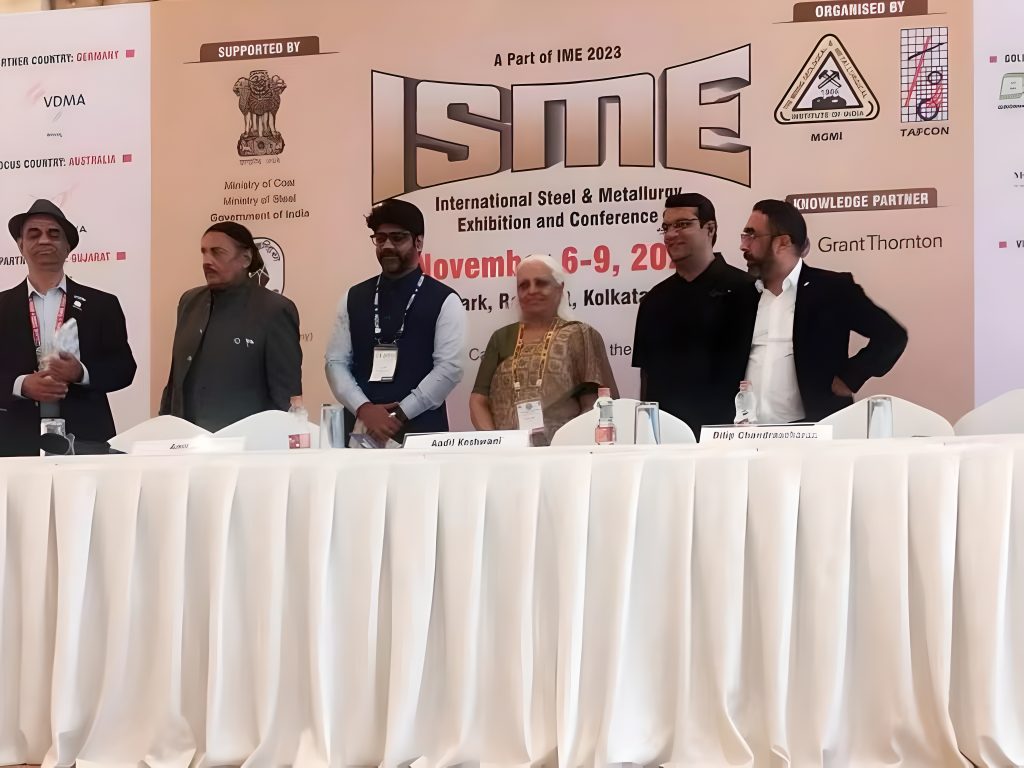
At John Finlay, we are thrilled to have been invited as a guest speaker at the prestigious IME 2023 Exhibition Mining Expo_IME , where We had the opportunity to present an insightful use case of AI and ML in the realm of mineral beneficiation technology. During our presentation, we shed light on the transformative potential of these cutting-edge technologies in optimizing the processing of vital resources such as iron ore, coal, lead zinc, and manganese ore. This is a step towards a green future. With the use of AI and ML at John Finlay we are able to introduce dry separation which not only saves water but reduces use of harmful chemicals and saves capex and opex costs at the same time saving the environment. We are excited to share the glims of my presentation with you all. Please stay tuned for the video, which will delve deeper into the innovative applications and benefits of AI and ML in this critical sector. #IME2023#MineralBeneficiation#AIinMining#MLInnovation#IronOre#Coal#LeadZinc#ManganeseOre#coalmining#mineralprocessing ##mineralbeneficiation#coalwashry#coalindia#coalbeneficiation#coal#ironoreAadil Keshwani

IME Exhibition 2023 Read More »